A Piece of Wood Far Below Ground: How Artesis e-MCM Found a Submersible Pump Fault From the Control Panel
Artesis case: an e-MCM unit in the control panel of a 3.3 kV deep well pump flagged unbalance and looseness. The SCADA vibration sensor confirmed 4.54 mm/s rms, and when the pump was pulled, a piece of wood was found jammed in the impeller.
Deep well pumps are the textbook case of "out of sight, out of mind". The motor and pump sit far below ground, submerged in the water they lift. Nobody can walk up to them with a vibration pen or put a hand on the casing. For the water utility running this 3.3 kV submersible pump, the only way to know its condition was to listen to what came up the cable.
That is what the Artesis e-MCM unit in the motor control panel did. One day it raised a warning.
Source. Case published by Artesis Technology Systems in October 2026. The manufacturer does not name the utility or the site.
The investigation
The e-MCM report showed a high unbalance level, along with looseness and rotor-related indications. The team checked this against SCADA, which had a separate online vibration sensor on the pump casing. It confirmed the diagnosis: 4.54 mm/s rms on the Z-axis at the suction side, clearly elevated.
The pump was pulled and inspected. The cause was in the impeller: a piece of wood had been sucked in and jammed between the vanes. It had dented the impeller and thrown the rotating assembly out of balance. The crew removed the debris and dealt with the damaged impeller.
For the supervisor, the best part was simple. "We didn't have to guess," he said. "The motor told us something was wrong with the pump, not with itself."
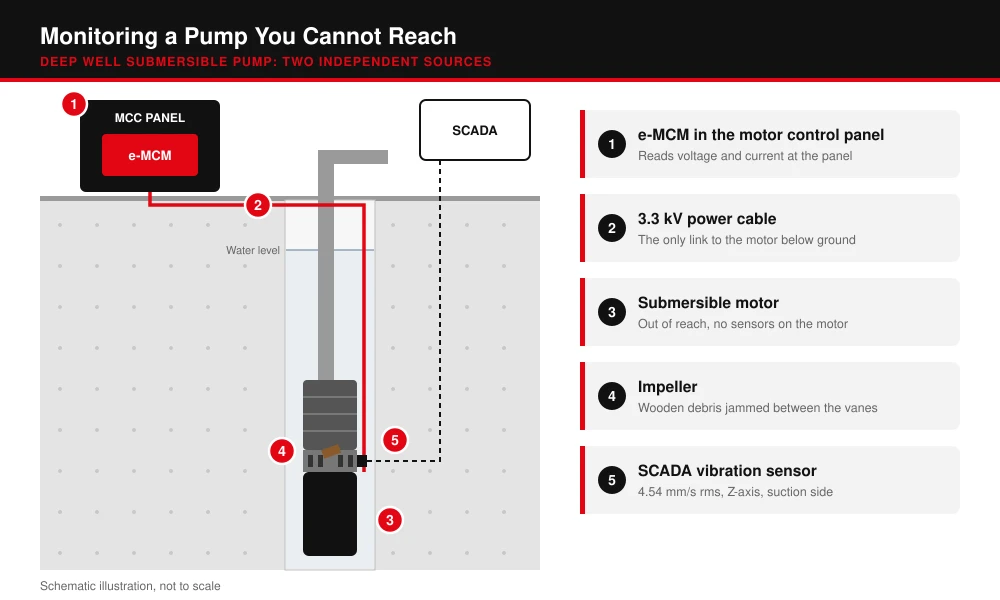
On the diagram (schematic, not to scale):
- e-MCM in the motor control panel reads voltage and current at the panel.
- 3.3 kV power cable is the only link to the motor below ground.
- Submersible motor is out of reach, with no sensors on it.
- Impeller has wooden debris jammed between the vanes.
- SCADA vibration sensor reads 4.54 mm/s rms, Z-axis, suction side.
Two independent sources, the electrical signature and vibration, pointed to the same thing. That made the decision to pull the pump an easy one.
What are driven equipment faults?
These are problems in the machine the motor drives, not in the motor itself. Examples:
- Pumps: damaged, eroded or blocked impellers, worn wear rings, vane damage, rubbing, bent shafts.
- Fans: blade erosion, build-up, cracked or loose blades, hub problems.
- Compressors: valve leaks, worn pistons or rings, rotor rub.
- Mixers, mills, conveyors: worn scrapers, damaged paddles, changes in process load.
The motor delivers all the torque the driven machine needs. So every irregularity in that machine shows up as a small modulation of the motor current. Electrical signature analysis turns the motor into a sensor for the whole drive train.
Equipment covered in this article
Artesis e-MCM — Online Sensorless Motor Monitoring
Online sensorless electric motor monitoring with AI and digital twin
How driven equipment faults develop
- Foreign objects entering pumps or fans, as with the wood in this case.
- Erosion and corrosion from abrasive or aggressive fluids.
- Cavitation damage on pump impellers.
- Dust or product build-up on fan blades.
- Fatigue cracks from long-term cyclic loading.
- Wear of close-clearance parts: wear rings, seals, compressor valves.
What they lead to
- Unbalance and vibration, which in turn damage bearings and seals.
- Loss of hydraulic or aerodynamic efficiency, so more energy per unit of output.
- Reduced capacity: less flow, pressure or airflow.
- Eventually a catastrophic failure: a broken impeller or a thrown fan blade.
Correlations to look for
| Indications in the report | Likely cause |
|---|---|
| Driven equipment + unbalance | Blade or impeller damage, debris or build-up |
| Driven equipment + load change | Blockage, wear or a change in the process |
| Driven equipment + flow turbulence / cavitation (pumps) | Hydraulic problems at the impeller |
| Driven equipment rising only when a second machine runs | Interaction in shared ducts or headers |
Checklist for maintenance and CM staff
- Compare the motor current or active power trend with process data: flow, pressure, level.
- Check inlet screens, strainers and suction areas for debris.
- Correlate with existing vibration or SCADA data. Two independent sources give confidence.
- For fans, schedule blade inspection and cleaning when unbalance and driven equipment trends rise together.
- After a repair, re-learn or re-baseline the monitoring if the machine's behaviour has changed significantly.
Key takeaways
- Driven equipment faults can be detected from the motor control panel, even on submersible pumps you cannot reach.
- Unbalance on a pump often means something is physically wrong in the impeller.
- Combining e-MCM with SCADA data gives fast, confident decisions.
For a full picture of pump station monitoring with SDT ultrasound and Artesis drive monitoring, see the article on water utility pump stations.
KEG TRK is the official Artesis distributor in Kazakhstan. Running borehole, submersible or other hard-to-reach pumps? Talk to us about monitoring them with e-MCM straight from the control panel.
Equipment in this article
KEG TRK quotes prices and delivery times to Kazakhstan on request. We will prepare a commercial offer for your application.
Artesis e-MCM — Online Sensorless Motor Monitoring
Online sensorless electric motor monitoring with AI and digital twin
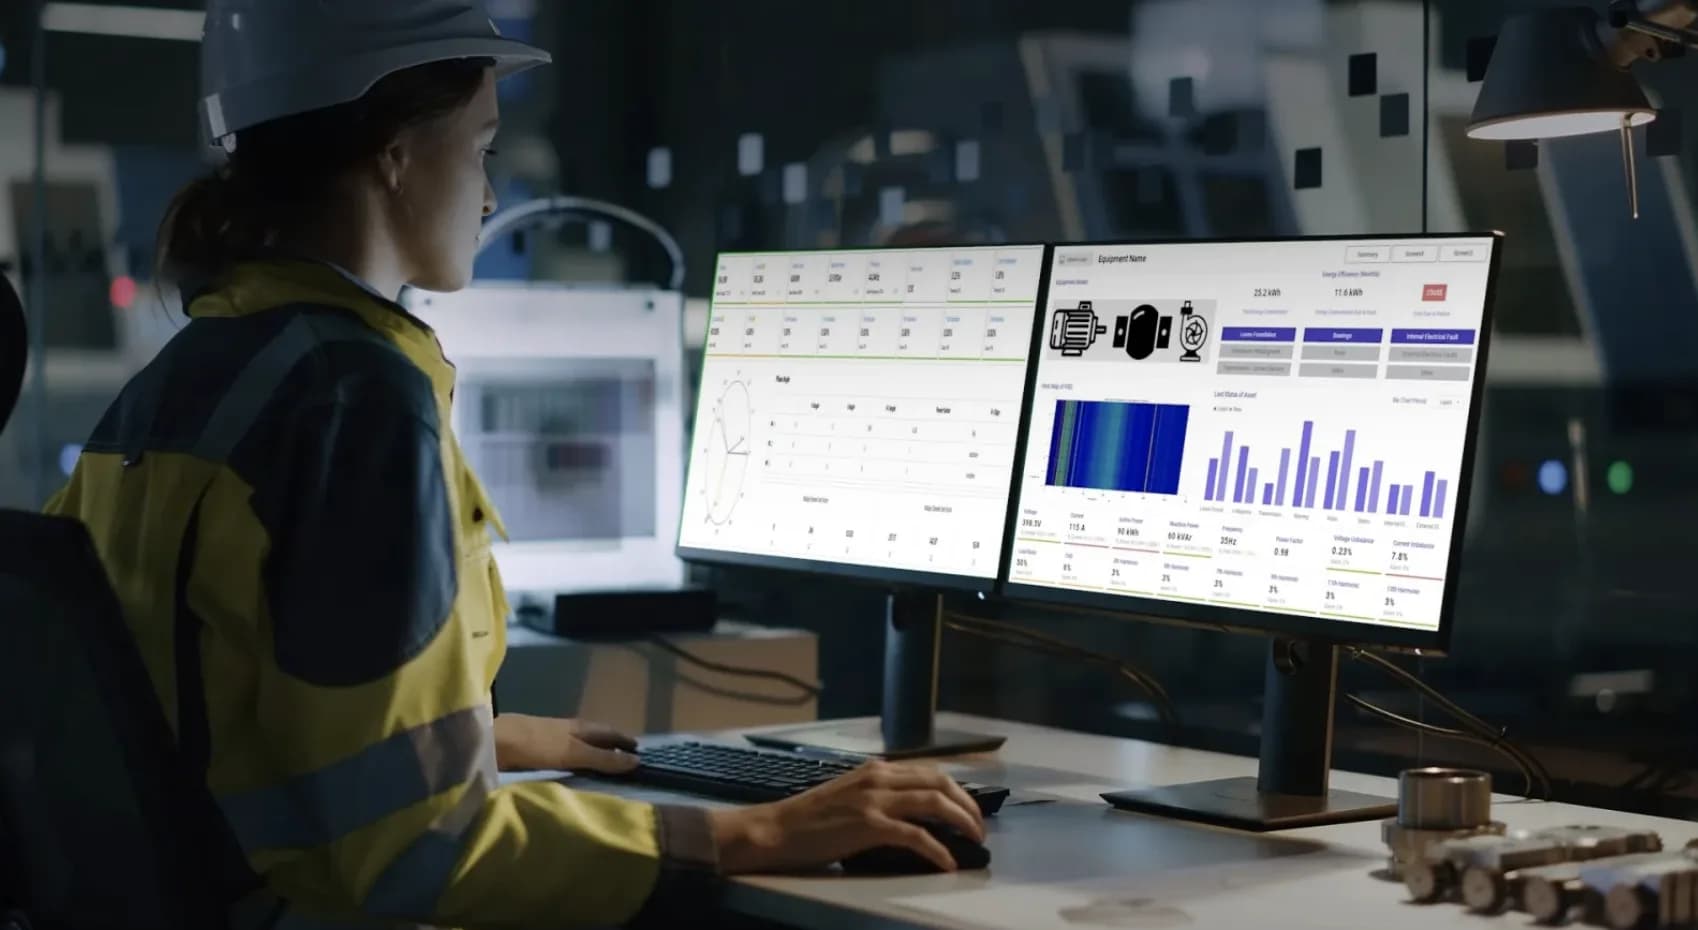
Artesis IoT — Cloud Monitoring Platform
Cloud platform for monitoring data management, analytics and reporting
Read also
6/18/2026
Case Study: Online Monitoring of 120 Motors and Artesis e-MCM Payback
A typical Artesis e-MCM deployment case: 120 critical motors, two prevented failures, loss calculations, and system payback in under a year.
10/6/2026
Shaft Seals and Suction: Catching Air Ingress and Dry Running in Pumps
Packing or mechanical seal, flushing, air ingress in the suction line and dry running: how it works, how it fails, and how to detect the problem with SDT340 ultrasound and Artesis electrical signature analysis.
6/30/2026
Case Study: 12-Month PdM Rollout at a Mine and CHP — Artesis, Bently and SDT
Typical holding scenario: SDT routes, Orbit DCM on conveyors, e-MCM on mills, e-PCM on DGS, IoT for management — timeline, metrics and lessons.